
 English
 русский
 Español


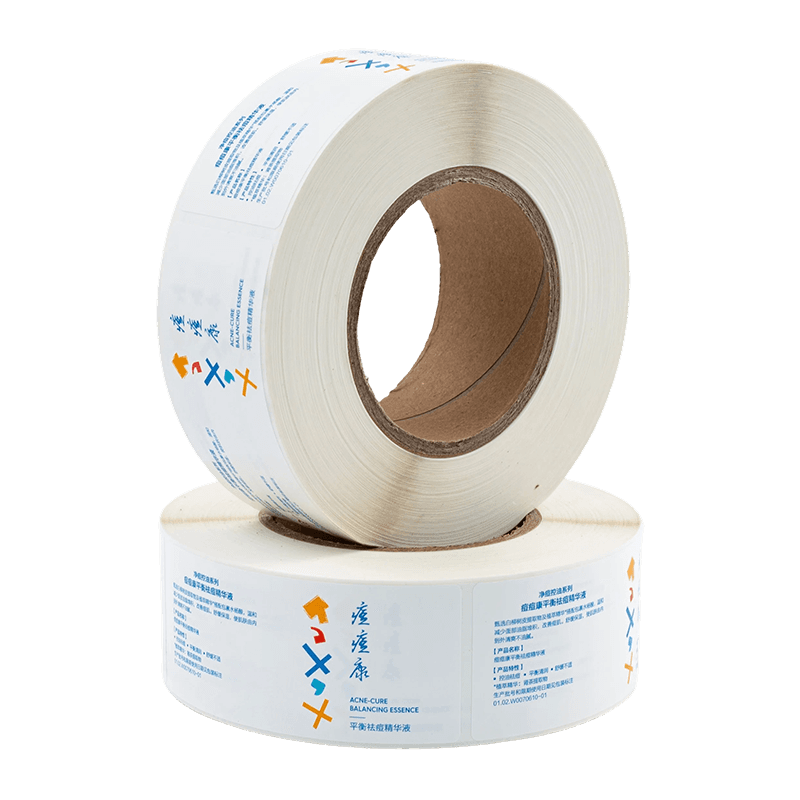

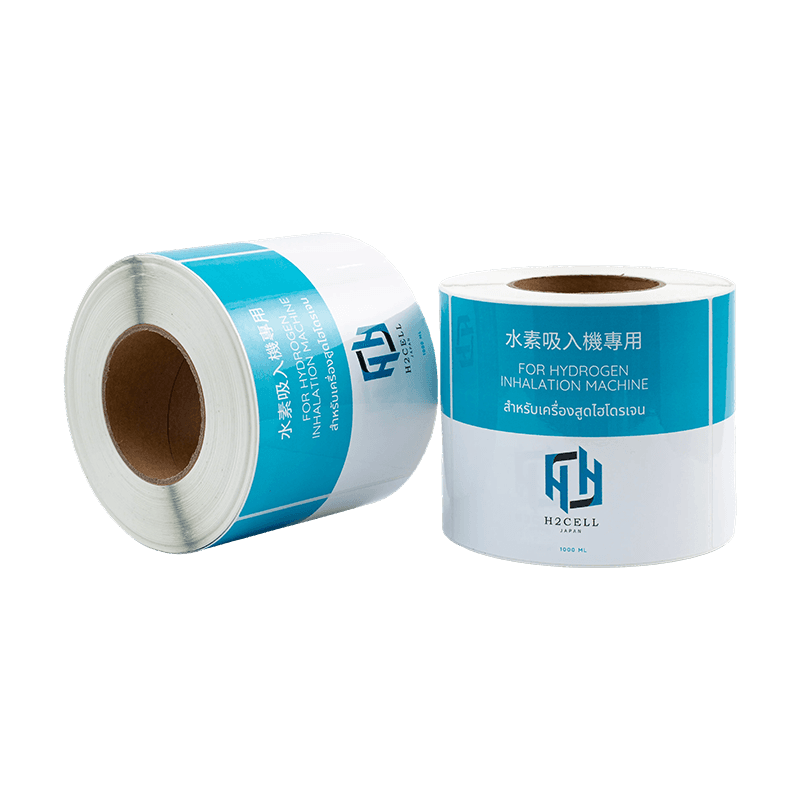
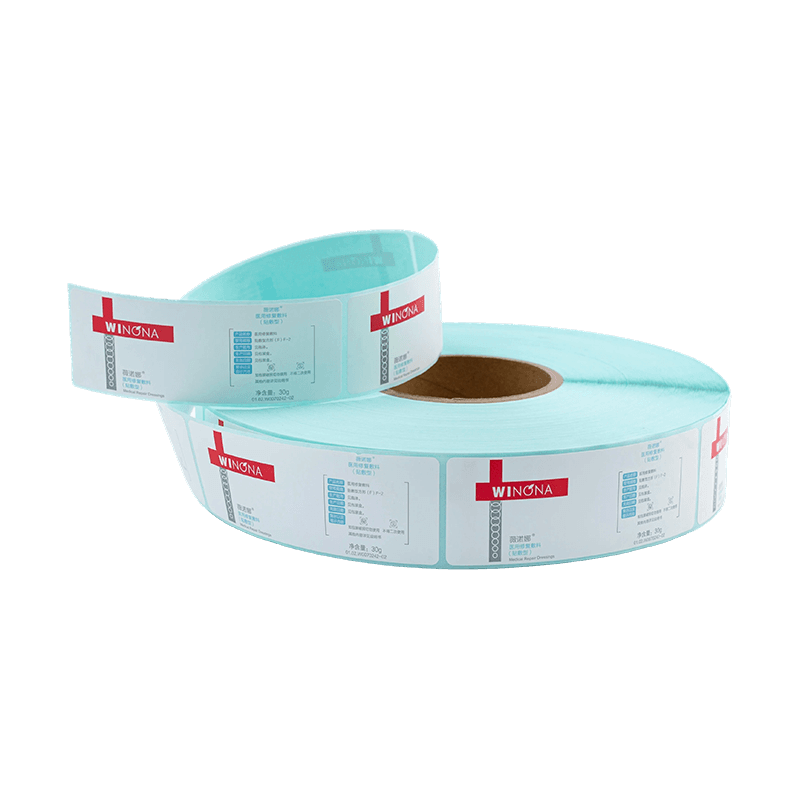
Healthcare labels are the lifeline connecting products, healthcare professionals, and patients, and the cornerstone of the safe and effective use of medical devices and pharmaceuticals. These labels transcend the scope of traditional labeling, meeting the most stringent global regulatory standards (such as FDA 21 CFR Part 11, EU MDR, ISO 13485, GMP), providing absolutely reliable information delivery and physical performance under extreme sterilization, long-term implantation, complex pharmacological environments, and stringent traceability requirements. Their core value lies in ensuring zero errors throughout the entire process from production, sterilization, warehousing to clinical use, under extremely miniaturized or demanding conditions, through the integration of materials science, adhesive technology, and precision printing.
In terms of materials and safety, the requirements are paramount. Labels that come into direct or indirect contact with pharmaceuticals, devices, or the human body must use medical-grade, hypoallergenic, and biocompatible materials, such as pure polypropylene (PP), polyethylene (PE), polyester (PET), or specialty polyimide films, combined with pressure-sensitive adhesives that have passed USP Class VI or ISO 10993 biocompatibility testing. For sterile packaging, materials must withstand various sterilization methods, including gamma irradiation, ethylene oxide (EO), autoclave, and electron beam sterilization, while maintaining stable performance, clear information, and no release of toxic substances.
Core performance is built around extreme reliability and information integrity. Labels must possess exceptional chemical resistance to withstand repeated wiping with alcohol, isopropanol, disinfectants, and pharmaceutical solvents; excellent temperature and weather resistance to adapt to cold chain (-80°C), high-temperature sterilization (above 135°C), and various storage environments; and extremely high dimensional stability and adhesive durability to ensure no warping or detachment throughout the device's lifespan. Furthermore, tamper-evident/void-detection (VOID) functionality is crucial for ensuring aseptic barrier systems and drug safety, while serialization and UDI (Unique Device Identifier) coding are mandatory technologies to meet global regulatory traceability requirements.
Product highlights include customized solutions for complex application scenarios. For example, tiny tubular instrument tags can be clearly printed on catheters with a diameter of less than 1 mm; sterilizable RFID tags can be embedded in instrument trays to automate warehousing and operating room management; soluble tags are used in multi-step medication dispensing processes; and implant tags need to remain stable in the human body for a long time. From ensuring the cold chain traceability of every vaccine to ensuring the absolute sterility of every surgical instrument pack, healthcare tags, with their scientific rigor, silently safeguard life, health, and safety, and are an indispensable high-tech and highly compliant component of the medical industry.
About Rongyang
Shanghai Rongyang Industrial Development Co., Ltd.
Shanghai Rongyang Industrial Development Co., Ltd. is a leading integrated solutions provider of pressure-sensitive labels and RFID smart labels in China. Healthcare Labels Manufacturers. Integrating R&D, manufacturing, sales, and service, the company is dedicated to delivering high-quality, diversified, and innovative label products and technical services to global clients.
Since its establishment, Rongyang has consistently adhered to a market-oriented approach driven by technology. We are Healthcare Labels Factory in China. In the manufacturing sector, we possess advanced fully-automated production lines, precision inspection equipment, and a stringent quality control system, ensuring every step from raw materials to finished products meets excellent standards. Our core products encompass:
• Pressure-Sensitive Labels: Including general-purpose, weather-resistant, and special material labels, widely used in industries such as fast-moving consumer goods (FMCG), food & beverage, pharmaceuticals, logistics, and retail.
• RFID Smart Labels: We supply RFID inlays, tags, and finished products in various frequencies, including High Frequency (HF) and Ultra-High Frequency (UHF). Our RFID solutions empower sectors like warehouse logistics, asset management, retail anti-theft, and smart manufacturing, facilitating digital and intelligent transformation for enterprises.
As a top-tier supplier in the industry, we go beyond offering standard products by focusing on delivering customized solutions. Leveraging our robust R&D team and flexible production capabilities, we can respond swiftly to client needs, designing and manufacturing label products that meet specific application scenarios and possess special functions (such as anti-counterfeiting, high-temperature resistance, removable adhesion, etc.).
Our vision is to become a trusted partner in the global label industry. Wholesale Healthcare Labels. Upholding the philosophy of "Continuous Improvement, Innovation, and Mutual Success," Shanghai Rongyang Industrial Development Co., Ltd. will persistently enhance product competitiveness and service value, striving to create shared value with our customers and lead the future of label applications.
-
2008
Founded in 2008
-
22000㎡
Factory Cover
-
3000000㎡
Production Volume (per month)
-
100000㎡
Export Volume (per month)
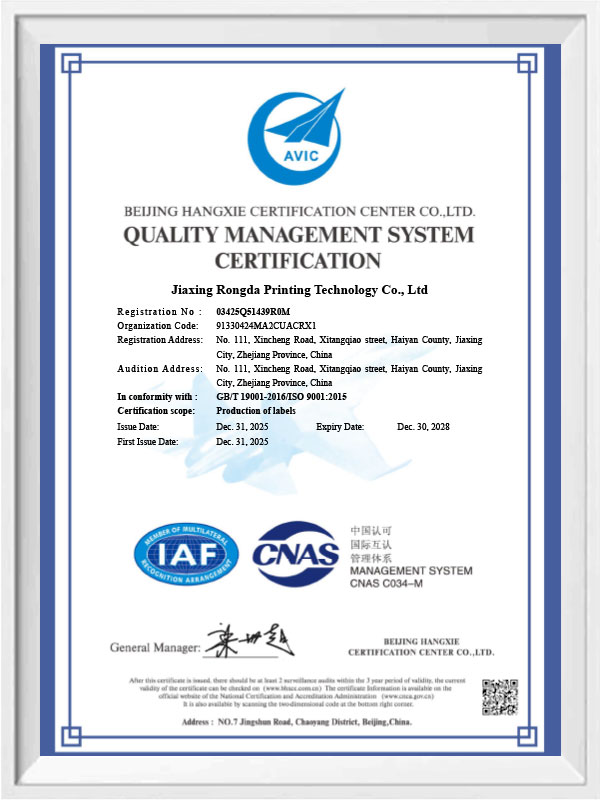
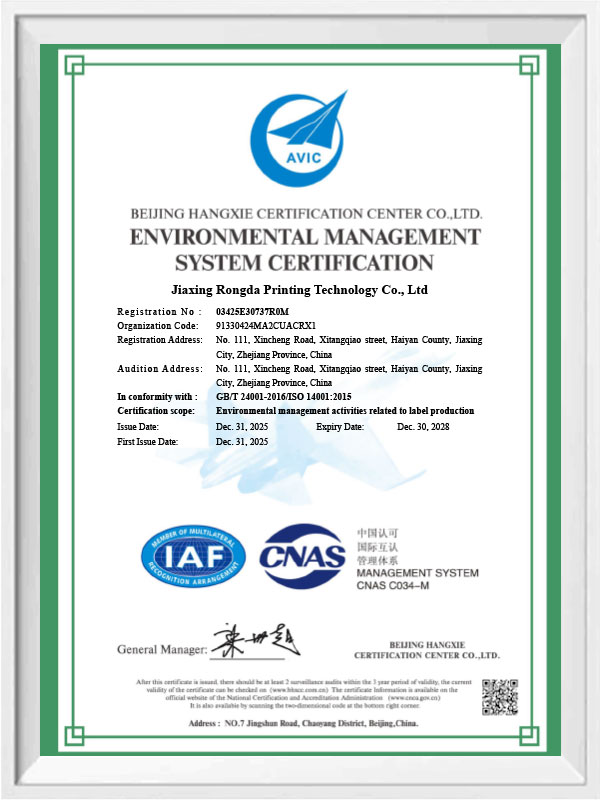
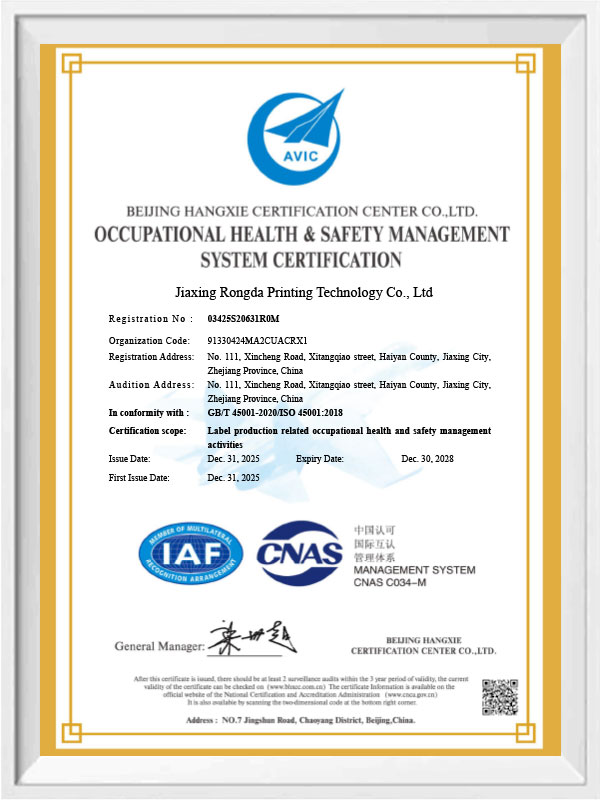
Certificate

News & Blog
Industry Trends & Tech Insights, Stay Updated with Label Innovations
Healthcare Labels Manufacturer
Shanghai Rongyang Industrial Development Co., Ltd. is a Healthcare Labels manufacturer and supplier in China, specializing in pressure-sensitive labels for medical devices, pharmaceuticals, and laboratory storage. Our range covers four core product families: medical device and pharmaceutical labels, specialty sterilization-resistant labels, medical-grade container labels, and ointment/gel tube labels. We serve global pharmaceutical companies, medical device OEMs, hospital supply chains, and diagnostic laboratories that require regulatory-compliant, high-performance labeling under demanding conditions.
Our healthcare labels factory in Haiyan, Zhejiang, operates automated production lines with precision inspection equipment, supported by ISO 9001, ISO 14001, and ISO 45001 certifications. We combine material science, adhesive technology, and precision printing to deliver labels that maintain integrity through sterilization, cold chain, chemical exposure, and long-term storage.
Our Healthcare Label Range
We offer four specialized label categories, each engineered for distinct clinical and pharmaceutical applications:
| Product Category | Key Applications | Critical Properties |
|---|---|---|
| Medical devices and pharmaceuticals Pressure-sensitive labels | Pharmaceutical bottles, medical device packaging, record forms | Medical-grade paper/film, biocompatible adhesive, excellent printability |
| Specialty product labels | Reusable surgical instruments, implant packaging, high-end diagnostic equipment | Polyimide, high-temp polyester, ceramic coatings; withstands autoclave, EO, gamma, plasma |
| Medical-grade container labels | Lab sample tubes, pharmaceutical storage bottles, bioreactor bags, cryopreservation boxes | USP <661>, ISO 10993 compliant; resistant to refrigeration, freezing, liquid nitrogen, disinfectants |
| Ointment/Gel Tubes Packaging Labels | Flexible tubes for ointments, gels, and semi-solid pharmaceuticals | Highly flexible PE/PP film, strong migration-resistant adhesive |
Application Fit and Material Considerations
Selecting the correct healthcare label depends on the container material, sterilization method, storage environment, and regulatory requirements. Our engineering team evaluates each project based on:
- Substrate compatibility: Labels must bond securely to glass, plastic, or coated surfaces without lifting or ghosting.
- Sterilization tolerance: For reusable instruments, labels must survive repeated autoclave cycles above 132°C, EO gas, gamma irradiation, or plasma sterilization without loss of adhesion or readability.
- Chemical resistance: Labels on containers exposed to alcohol, isopropanol, or disinfectants must resist smearing and degradation.
- Temperature extremes: Cold chain labels must perform at -80°C, while sterilization labels must endure high heat.
- Biocompatibility: For direct or indirect contact, materials and adhesives must meet USP Class VI or ISO 10993 standards.
Critical Specifications and Performance
Our labels are engineered to meet the following performance criteria:
- Adhesion durability: No warping or detachment throughout the device's lifespan.
- Dimensional stability: Labels maintain size and shape under extreme conditions.
- Print clarity: High-resolution printing for barcodes, UDI codes, and lot numbers.
- Tamper-evident options: VOID features for aseptic barrier integrity.
- Traceability: Support for serialization and UDI coding to meet global regulatory requirements.
Configuration and Customization
We provide deep customization to match your specific application. Our capabilities include:
- Material selection: Choose from PP, PE, PET, polyimide, or ceramic-coated substrates.
- Adhesive systems: Permanent, removable, or low-temperature adhesives tailored to your container.
- Printing technologies: Flexographic, offset, letterpress, and HP digital printing for variable data.
- Special features: RFID integration, anti-counterfeiting, scratch-off, or temperature-sensitive inks.
- Die-cutting: Custom shapes and sizes, including tiny labels for catheters or micro-tubes.
Quality Assurance and Compliance
Our quality system is built on ISO 9001, ISO 14001, and ISO 45001 certifications. As one of the more established healthcare labels manufacturers in the region, we operate a professional testing laboratory equipped with:
- RFID performance integrated tester
- High/low temperature and humidity test chamber
- Tensile testing machine
- Chemical resistance testing equipment
- Barcode scanner and verifier
Every batch undergoes strict raw material inspection, in-process monitoring, and finished product testing. We maintain full traceability from raw material batch to production group and test data.
Information We Use to Configure Your Solution
To prepare an accurate proposal, our engineers need the following project details:
- Application: Type of medical device, pharmaceutical, or container.
- Container material: Glass, plastic type, or coated surface.
- Sterilization method: Autoclave, EO, gamma, or other.
- Environmental exposure: Temperature range, chemicals, humidity.
- Regulatory requirements: FDA, EU MDR, ISO 13485, or other standards.
- Printing needs: Variable data, barcodes, UDI, graphics.
- Volume and size: Annual quantity, label dimensions, and roll format.
Frequently Asked Questions
Can you produce labels that withstand repeated autoclave sterilization?
Yes, our specialty product labels are designed for reusable surgical instruments and implant packaging. They withstand autoclave temperatures above 132°C, EO gas, gamma rays, and plasma sterilization, maintaining adhesion and readability after multiple cycles.
Do you offer labels for cryogenic storage?
Our medical-grade container labels are suitable for refrigeration, freezing, and liquid nitrogen storage. They are made with medical-grade plastics and adhesives that remain stable at ultra-low temperatures and resist disinfectant wiping.
Can you print UDI codes and variable data on healthcare labels?
Yes, we support serialization and UDI coding using digital and flexographic printing. Our quality control includes barcode verification to ensure accuracy and compliance with global traceability standards.
What certifications do you hold for healthcare label manufacturing?
We are ISO 9001, ISO 14001, and ISO 45001 certified. Our materials and adhesives can be selected to meet USP Class VI or ISO 10993 biocompatibility requirements as needed for your application.
How do you ensure label performance in chemical environments?
We test our labels for resistance to alcohol, isopropanol, and common disinfectants using chemical resistance testing equipment. We select materials and adhesives that maintain integrity under repeated wiping and exposure.
Messae Us Right Now!
- Quick Links
- Products
- Quality Control
- Our Story
- News
- Contact
- Our Product
-
- Beauty and Personal Care Labels
- Home cleaning and laundry care labels
- Liquor and Beverage Labels
- Food and dairy product labels
- Healthcare Labels
- Promotional and Interactive Labels
- Specialty and industrial solution
- Labels Thermal printing and logistics labels
- Anti-counterfeiting traceability and RFID Labels
- Contact us
- Tel:+86-573-86867861
- Phone:+86-18621872035
- E-mail:allen.men@rylabel.com
- Add:No. 111 Xincheng Road, Haiyan Economic Development Zone, Jiaxing City, Zhejiang Province


